Break the Dewpoint Addiction.
Dry Air is Not Dry Plastics.
- Every resin dryer in the world is sold on one number: dewpoint. It tells you the dryer is working.
- It’s a performance check on the machine — like temperature or airflow. It says nothing about the condition of the pellet coming out the bottom of the hopper.
- That is an addiction. This is the intervention.
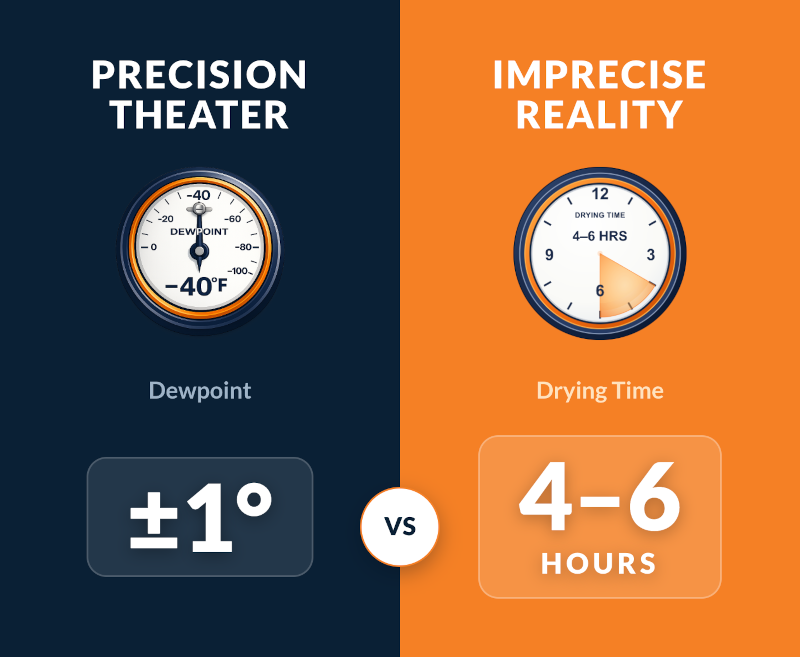
One written like a Swiss watch. One written like a weather forecast.
The Outlier Industry
Every Serious Process Industry Measures Incoming Moisture. Except One. Why?
✓CONCRETE
Measures aggregate moisture daily and corrects the batch water for it.
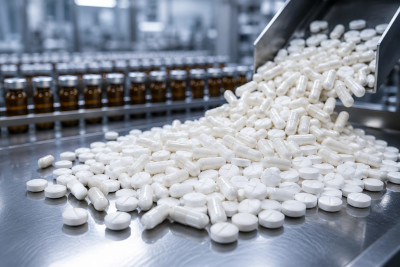
✓PHARMA
Moisture-tests every incoming lot to a hard spec before release.
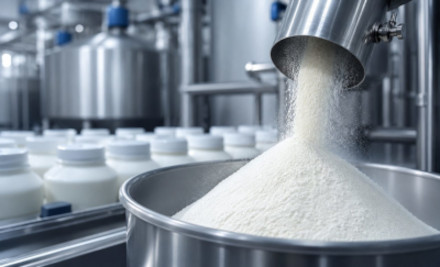
✓DAIRY
Spray-dries milk powder to a measured endpoint. Every batch verified.
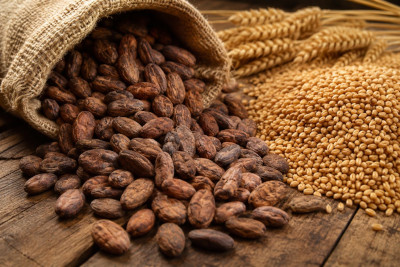
✓COCOA & GRAIN
Rejects a whole lot over two points of moisture. Above that line, it rots.
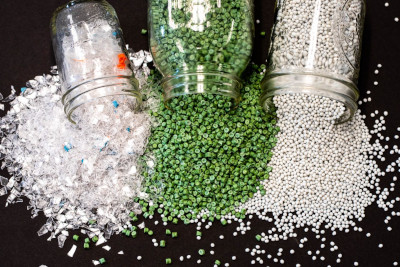
✗PLASTICS — THE OUTLIER
Runs dollar-a-pound resin into a dryer without knowing its starting moisture.
For forty years, measuring the moisture inside a pellet was either impossible on the plant floor or too expensive to justify. So the industry measured what it could reach — the air — and the stand-in became the standard. Now, it’s possible.
We built a religion around the dryness of the air — and turned the moisture in the resin, the only number those industries would accept as the answer, into the one thing nobody measures.
The Good News
The variables that actually make dry plastic are knowable, measurable, and controllable. We’ll get there. But first you have to see the addiction clearly.
The Precision Double Standard
A “Precision” Process, Specified in the Sloppiest Possible Terms
- The number the industry does measure gets single-degree resolution, alarms, and a trend line. The dewpoint spec is sold with the swagger of precision — as if that decimal point on the readout were proof of a serious machine.
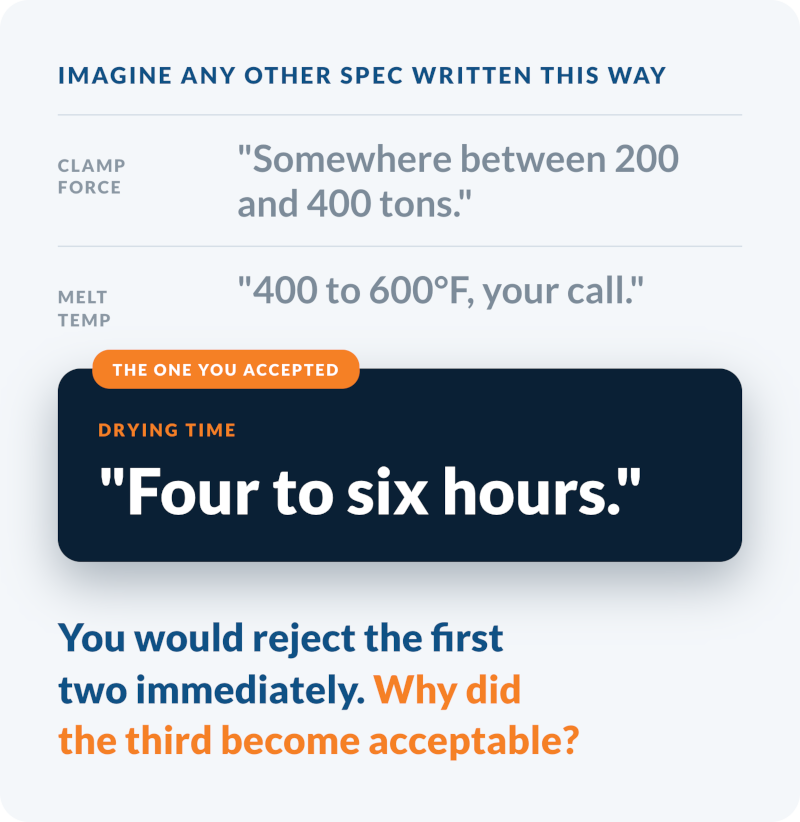
- Ask about drying time — the variable that actually determines your final ppm — and the same industry hands you a range you could drive a truck through. A ±50% tolerance on the single most important input to your result.
- Ten feet away, your molding press is profiled in fractions of an inch per second, pressure to the psi, cycle time to the hundredth of a second.
Imagine specifying that press the way we specify drying: “run the cycle somewhere between 4 and 6 seconds.” You’d never accept it — not for a single shot.
A process is not precise because one convenient variable is measured precisely. It is precise because the variable that controls the outcome is controlled precisely.
The Same Dryer. The Same Resin. Two Very Different Days.
Same Dewpoint. Same Ending
Moisture. One Load Took Twice as Long.
RESINNylon 6— incoming moisture swings hardest with the season
Twice the drying time — and nothing on the dryer changed.
Why?
Starting moisture.
- Drying is diffusion: bound water, liberated by heat, migrating slowly to the surface. How long that takes depends on how much water is in the pellet to begin with — and that number changes with the season, the packaging, and the resin’s history.
- Now look again at the spec from the top of this page: “four to six hours.” That range isn’t engineering tolerance. It’s an admission — the industry writes drying time as a window because it never knows the starting moisture. Measure what goes in, and the window collapses to a number.
Dry air is permission to dry. It is not drying.
Why the Industry Fed the Addiction
The Dewpoint Gauge Should Be Three Lights, Not a Dial
Dewpoint became the universal spec because it’s the only common denominator — cheap to instrument, easy to advertise. Then the industry sold you more of it: −60, −80, −100°F marketed as premium, when below −40°F there is little measurable drying benefit for the vast majority of resins. A premium price for a bigger electric bill.
Temperature inside the hopper
tough to measure
nobody does
Airflow at the pellet
tough to measure
nobody does
Dewpoint of the air
tough to measure
on every panel in the world
The industry didn’t measure what matters. It measured what was convenient — then declared it what matters.
What do you actually need from a dewpoint reading? One thing: is the air system healthy or not? That’s a status light, not a performance meter — the oil-pressure light of drying.
GREEN
The desiccant system is doing its job. The air is dry enough. Carry on.
YELLOW
Dewpoint is drifting up — desiccant saturating, filter clogging, regeneration lagging. Investigate before it bites you.
RED
The air system has failed. Stop and fix it.
We were all taught to pay attention to the variable that is easiest to sell instead of the variables that make dry plastic.
Getting Clean
The Three-Step Detox
Breaking the habit doesn’t require throwing out the dewpoint gauge. It requires putting it back in its place — a vital sign of the desiccant system, nothing more.
THE VARIABLE EVERYTHING ELSE DEPENDS ON
1
Treat the incoming resin like the expensive ingredient it is.
Assume nothing is dry on arrival. Know your starting moisture the way a concrete plant knows its aggregate. Everything downstream — the dryer, the drying time, the result — is built on this number. This is where the page began: the outlier industry, made un-outlier, one plant at a time.
2
Stop grading your dryer only on the dryness of the air.
Airflow carries heat to every pellet — keep it on the list. The dewpoint number only tells you the desiccant plumbing is healthy. Demote it to a green/yellow/red status light.
3
Put drying time at the top — in minutes, not hour-wide ranges.
A variable with a ±50% tolerance isn’t a spec, it’s a hope. Insist on controlled, verified residence time. Treat any “4 to 6 hours” as an admission the vendor can’t control the one thing that counts.
Dry air is not dry plastic. It never was. Break the addiction.
Like most problems in life, drying is complicated. Reducing it to one parameter — the dewpoint of the air — isn’t simplification. It’s sacrilege.
That’s the Intervention. The Full Science Lives Here.
The physics, the data, the criteria that actually matter — the complete technical argument, in the Novatec Knowledge Center.
The Print Edition
Take the Manifesto With You
The designed print edition — the full argument, laid out for the conference table. The web version stays free and open, always.
Published by Novatec, Inc. — home of the Novatec Tech Center, the only facility of its kind in North America: a working drying lab with Karl Fischer moisture analysis, ANSYS and Rocky simulation, and competitor equipment tested side by side.


SOURCES
Guidelines for Drying PET — PS Stoughton. Drying-curve data, diffusion physics.
The Low-Down on Dryer Airflow — Plastics Today. Temperature gradient, cold zones, effective residence time.
Overcoming Challenges of Feeding Bulk Solids — Processing Magazine. Funnel flow, ratholing, non-uniformity.
Guide to Specifying a Dryer — J. Bozzelli, Plastics Technology. Cone angles, rat-holing, dewpoint caveat.
Understanding Dew Point in Resin Drying — Novatec. Diminishing returns below −40°F; desiccant-health indicator.
Moisture Matters · You Must Dry Hygroscopic Resins — Plastics Technology. Seasonal swing; porous packaging.
Resin Moisture — Novatec. Nylon absorption range.
Aggregate Moisture Correction — NRMCA. Concrete batch-water correction.
Good Manufacturing Practices — Health Canada. Incoming raw-material testing and quarantine.
Cocoa Beans Guide — Eurococoa. Incoming-moisture rejection threshold.
Choosing the Right Dew Point Sensor — WiseAir. Capacitive sensor lag and recovery time.
