By Greg Washburn and Joshua Belisle · Edited by Dana Gardner
Published August 7, 2024 · Reviewed by Greg Washburn · September 7, 2026

Summary

How do I troubleshoot a vacuum pump at startup?

Start by checking the pump’s direction of rotation and motor amperage, then belts, blower wear and oil level. Next, block the cyclone inlet until the gauge reaches the pump’s maximum rated vacuum and the relief valve opens; if it can’t, there is an air leak at the dust collector, pump or piping. While conveying, the gauge should read between 4″ Hg and about 1″ Hg below the relief point.

Basic Startup / Troubleshooting Checklist – Vacuum Pump

  1. Check direction of rotation of the pump / motor. If incorrect, change phase.
  2. Check that motor amperage draws are correct. If not, check wire terminations at motor starter. Also check resistance across motor voltage legs, and between each leg and ground.
    • No resistance indicates shorted windings.
    • An open circuit between voltage legs indicates damaged windings.
  3. Check belts for proper tension and alignment, as well as wear and tear.
  4. Check blower for wear and tear, such as bearing play, leaking seals excess backlash.
  5. Check oil level in Positive Displacement and Claw pumps. Replace if necessary per Instruction Manual.

    NOTE: Regen pumps do not require oil changes but they should have their bearings lubed per instruction manual.
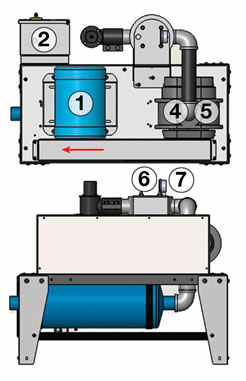
  6. Check pump and system vacuum capacity:

    a) Remove vacuum line from inlet to the cyclone (or central dust collector).
    b) Partially cap off the cyclone inlet with a rigid, flat object (wood, sheet metal, etc.).
    c) Begin operating the pump, and begin to slowly block more air at the cyclone inlet to increase the vacuum being drawn. The vacuum gauge should be able to reach maximum inches Hg vacuum for the pump (see pump instruction manual). This will let you know the pump is sealed properly. Confirm the high vacuum relief valve opens to prevent pulling more than maximum rated vacuum.

    • If the vacuum level fails to reach maximum, there is an air leak at the dust collector or pump. Check the seal on the dump can on the cyclone, the filter housing lid seal at the pump, the vacuum breaker valve, (verify it has air 85 to 100 psi), and all piping connections.

    d) If the maximum vacuum is reached, and the relief valve functions properly, reconnect the vacuum line to the system and perform another vacuum check. If maximum vacuum is reached, and the relief valve functions properly, the system is sealed and all station vacuum valves are closed.

    • If the valve doesn’t open, you have a system vacuum leak. Check for any open lines, open system vacuum valves (Station T Valve or lid mounted External Fill Valve), or loss of compressed air to system vacuum valves.
  7. Check the vacuum while the system is conveying material. Normally, the pump vacuum gauge should read between 4” Hg vacuum and up to 1” Hg less than the pump relief point. Typically, vacuum<4” Hg indicates a vacuum leak or no movement of material. Vacuum >relief point can be caused by:
    • Line clogging where too much material is in the conveying line without the proper air mixture.
    • Stations are being overfilled.
    • The filter on the vacuum chamber or at the pump may be clogged.
    • The station vacuum valve may not be opening (check control settings and the valve itself).
Frequently Asked Questions

What vacuum should a conveying pump read while moving material?

The pump gauge should normally read between 4″ Hg and up to 1″ Hg less than the pump’s relief point. A reading below 4″ Hg usually points to a vacuum leak or no material moving. A reading above the relief point can mean a clogged line, overfilled stations, a plugged filter at the vacuum chamber or pump, or a station vacuum valve that isn’t opening.

How do I find a vacuum leak in a conveying system?

Remove the vacuum line at the cyclone inlet, partially cap the inlet and run the pump. If the gauge won’t reach maximum vacuum, check the cyclone dump can seal, the filter housing lid seal, the vacuum breaker valve (85 to 100 psi air) and piping connections. If the pump passes, reconnect the line and repeat; failure then points to open lines, open station valves or lost compressed air.

Does a regenerative vacuum pump need oil changes?

No. Regenerative pumps do not require oil changes, but their bearings should be lubricated per the instruction manual. Positive displacement and claw pumps do use oil, so check the level at startup and replace it as the manual directs. Also check belt tension and alignment, and look for bearing play, leaking seals or excess backlash in the blower.

About the Authors

Greg Washburn, Novatec Vice President of Operations

Vice President of Operations, Novatec

Greg Washburn is Vice President of Operations at Novatec and has been with the company for more than three decades. He is involved in all phases of engineering design and product manufacturing, giving him a broad perspective on how resin drying and conveying equipment moves from engineering concept through production and into real-world processing environments. Greg holds a B.S. in Mechanical Engineering from the University of Maryland, Baltimore County (UMBC) and an MBA from Loyola University Maryland. His experience spans engineering, manufacturing and operations across Novatec’s material-handling technologies.

Joshua Belisle, Novatec Technology Manager

Technology Manager, Novatec

Joshua Belisle is Technology Manager at Novatec, where his work focuses on simulation and technology development for resin drying. He earned a B.S. in Mechanical Engineering with a minor in Engineering Business from the University of Virginia in 2023 and joined Novatec that same year. Joshua uses simulation tools to investigate previously difficult-to-measure aspects of the drying process, helping Novatec better understand airflow, heat transfer and other variables that influence resin-drying performance.

Related Articles

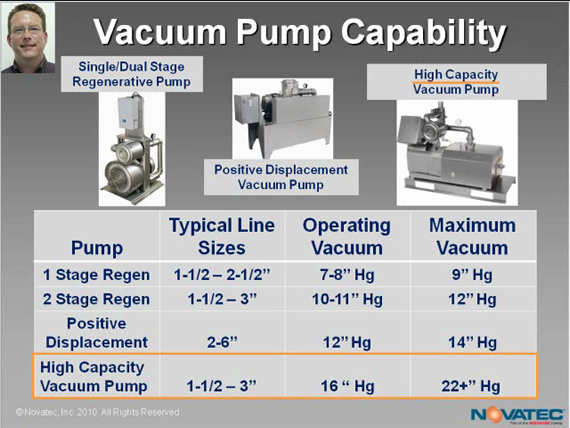
Compare vacuum pump types and the factors that guide selection for a plastics processing plant.

Compare vacuum pump technologies using the article’s pump comparison chart.

Learn how vacuum receivers operate and how to choose and maintain them for a conveying system.

Ask the Expert

Greg Washburn, Conveying Product Engineering Manager, Novatec, Inc.

Submit A Question

Novatec, Inc.

410-789-4811 | 800-237-8379

http://www.novatec.com

Scroll to Top